
A missing torque wrench can hold up far more than one job. It can delay a maintenance task, interrupt a production run, create an unplanned purchasing request and leave supervisors trying to establish who last had it. This manufacturing tool tracking case study looks at how a practical identification system can bring order to shared tools without creating another admin burden for the workshop.
The example is representative of the problems commonly seen in UK manufacturing environments: a busy site, tools moving between stores and workstations, and an asset register that exists but is not consistently updated. The solution was not a complicated new platform. It started with durable asset labels, a clear numbering structure and a process people could follow on a busy shift.
The problem: tools were recorded, but not controlled
The manufacturer operated a central tool store alongside several production areas. Engineers and operators could collect common hand tools, measuring equipment, power tools and specialist jigs when needed. Some items were high value; others were inexpensive individually but costly in aggregate when frequently replaced.
The business had a spreadsheet-based register containing most major tools. In practice, it did not answer the questions that mattered on the shop floor. Was the tool still on site? Which department had it? Was it due for calibration? Had it been returned after a job?
Paper sign-out sheets had been tried, but handwriting was inconsistent and sheets were often incomplete. Existing labels varied widely. Some had been printed in-house, some were handwritten, and some had lifted after exposure to oil, cleaning products or regular handling. A label that cannot be read or scanned is not an asset identifier for long.
The resulting costs were not limited to replacement purchases. Time was being lost searching cupboards, benches, vans and individual work areas. Managers also had little confidence in stocktake figures, while the maintenance team could not reliably identify measuring tools that required calibration or inspection.
Setting a workable tool tracking standard
Before ordering labels, the operations manager defined what the system needed to achieve. Each tool had to have a unique identifier, remain identifiable in normal industrial use and work with the company’s existing asset register. The labels also needed to be easy to scan with handheld devices already used for warehouse tasks.
A simple identifier format was chosen: a site code, tool category and sequential serial number. For example, a calibrated measuring device could be recorded as MFG-MEA-00472. This gave staff enough information to identify the item at a glance, while the unique number prevented duplicate records.
The label layout included the company name, a human-readable asset number, a Code 128 barcode and a short instruction to return the item to the tool store. The barcode was used for speed; the printed number remained essential when a scanner was unavailable or the label was partly obscured.
Why barcode choice mattered
The business did not need a QR code simply because QR codes are familiar. Its existing software and handheld scanners worked well with Code 128, which can hold letters, numbers and punctuation in a compact barcode. That made it a sensible fit for the chosen identifier format.
A QR code could have been useful if staff needed to open a web form, operating instruction or maintenance record from a mobile phone. For straightforward check-out and return activity, it would have added little value. The right barcode symbology depends on the equipment, software and process already in place, not on what looks most modern.
Choosing labels for the workshop environment
Material selection was treated as part of the tracking system, not a finishing detail. Tools are handled repeatedly, stored in metal cabinets, exposed to grease and wiped down during cleaning. Standard paper labels would have been a false economy.
The site selected hard-wearing polyester asset labels with a permanent industrial adhesive. The material provided a clean printable surface for the barcode and serial number, while the adhesive was suitable for the majority of painted metal, plastic and smooth equipment surfaces. Labels were supplied in a size large enough for reliable scanning, but small enough to avoid covering safety markings, operating controls or calibration labels.
Not every item accepted the same label. Textured handles, heavily contoured tools and areas exposed to very high heat required individual assessment. In a few cases, the identifier was applied to a protective case or assigned through an alternative marking method. This is an important trade-off: standardising labels improves efficiency, but forcing one material onto every surface can lead to premature failure.
For assets where unauthorised removal was a particular concern, the company also considered tamper-evident labels. These can leave a visible pattern or fragment when removal is attempted, making transfer to another item more obvious. They are useful as a deterrent and an audit aid, but they do not replace secure storage or good issue controls.
The rollout: label, verify, then issue
The first task was a physical tool audit. Teams gathered tools from the central store, maintenance cupboards and production areas, then checked each item against the existing register. Duplicate entries, obsolete records and tools marked as present but no longer found were dealt with before any new labels were applied.
Each verified tool received its asset label and was scanned into the register. Staff recorded the asset number, description, category, home location, condition and, where relevant, calibration or inspection date. Photographing high-value or unusual equipment alongside the record gave supervisors an additional reference when checking returns.
The rollout was staged by tool category rather than attempting to label everything in one day. Measuring instruments and high-value power tools came first because they had the clearest compliance and replacement-cost implications. Common hand tools followed, then jigs, fixtures and portable site equipment.
This approach avoided disrupting production and allowed the team to correct issues early. For example, labels initially placed near the base of several cordless tools were difficult to scan when stored in charging racks. The placement standard was adjusted before the next batch was labelled.
Making accountability practical
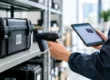
The new process was deliberately simple. Staff scanned a tool when collecting it and scanned it again when returning it. Where an item was issued for a longer job, the record showed the person, team or cost centre responsible and the expected return date.
Supervisors did not treat the system as a way to blame people for every misplaced screwdriver. The objective was to identify patterns: tools repeatedly left in a particular area, items that were requested more often than expected, and departments that needed a dedicated set rather than drawing from central stock.
That distinction helped adoption. Tracking works when people see it reducing delays and arguments, not when it feels like unnecessary surveillance. Managers still needed to follow up on unreturned equipment, but they could do so with a clear record rather than a general request sent to the entire shift.
What changed after the labels were in place
The most immediate improvement was visibility. Store staff could check whether a tool was available before searching for it, and shift supervisors had a more reliable view of items issued to their teams. Stock checks became a scanning exercise with targeted investigation, rather than a lengthy manual count based on faded or inconsistent markings.
The business also gained better purchasing information. If a particular tool was frequently unavailable, the manager could distinguish between genuine demand, a missing return or poor stock location. Buying an additional unit can be the right answer, but only after confirming that the existing tools are being tracked properly.
Calibration control improved because measuring equipment could be matched to its asset record quickly. Tools approaching their due date could be identified and removed from general circulation before they were used on quality-critical work. The label did not manage calibration by itself, but it made the process easier to enforce.
There were limits. Barcode labels rely on staff scanning at the point of issue and return, so training and supervision remained necessary. Labels also require occasional inspection, particularly on frequently handled tools. A damaged label should be replaced promptly and the replacement must carry the same verified asset identity, not a newly invented number.
Lessons for manufacturing sites
The case shows that tool tracking is most effective when the physical label, digital register and day-to-day working routine support one another. A detailed database cannot compensate for labels that fall off, and excellent labels cannot fix a process nobody follows.
Start with the tools that create the greatest operational risk: high-value equipment, calibrated instruments, portable power tools and items that move between departments. Define one numbering convention, choose a barcode your current system can read and test label adhesion on real working surfaces before committing to a full run.
Security-Label.co.uk can produce bespoke asset labels with serial numbers, barcodes, company details and materials selected for the intended environment. UK production and specialist advice make it easier to order labels that suit the job rather than settling for a generic office label.
The useful measure is not how many labels have been applied. It is whether the next person who needs a tool can find it, verify it and put it back into service without losing half an hour of production time.